
Defects are usually born at the receiving dock of the factory, not at the inspection bench near the end. Incoming material control â what the supplier checks before production starts â decides most of the quality outcome before a machine runs. This guide shows ptfe lined transport storage tanks buyers what to verify at the source.
Quality is decided earliest where nobody watches: at material intake. Buyers who shift attention upstream spend less on inspections downstream, and the arithmetic compounds every order.
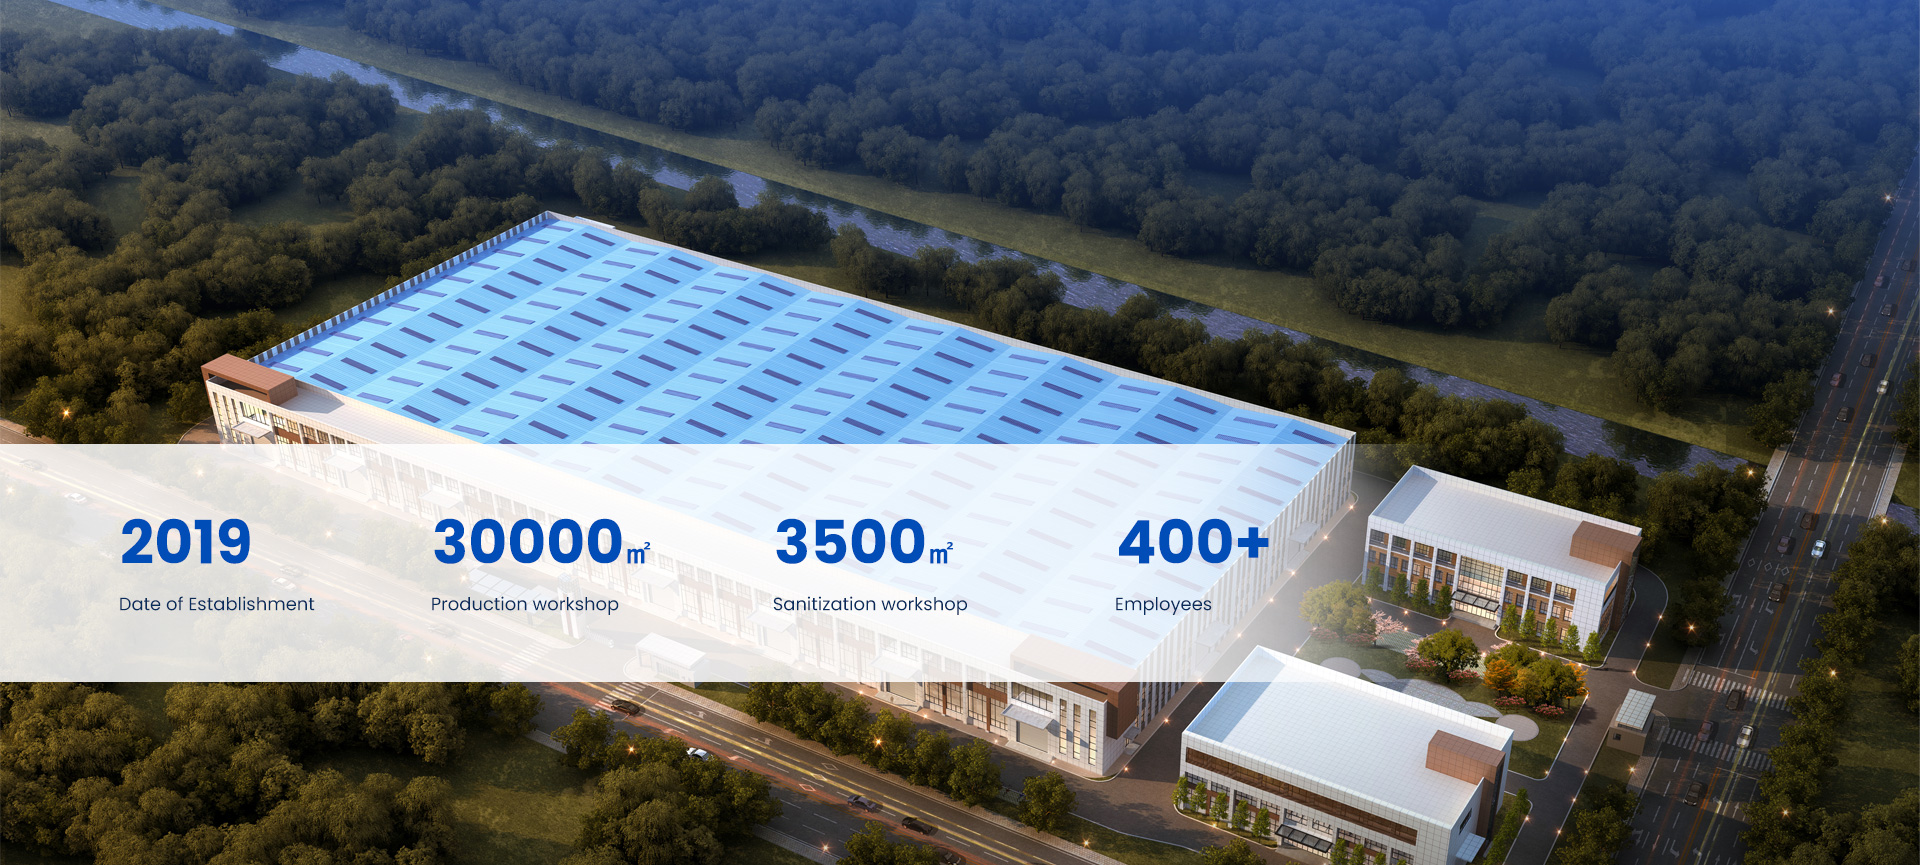
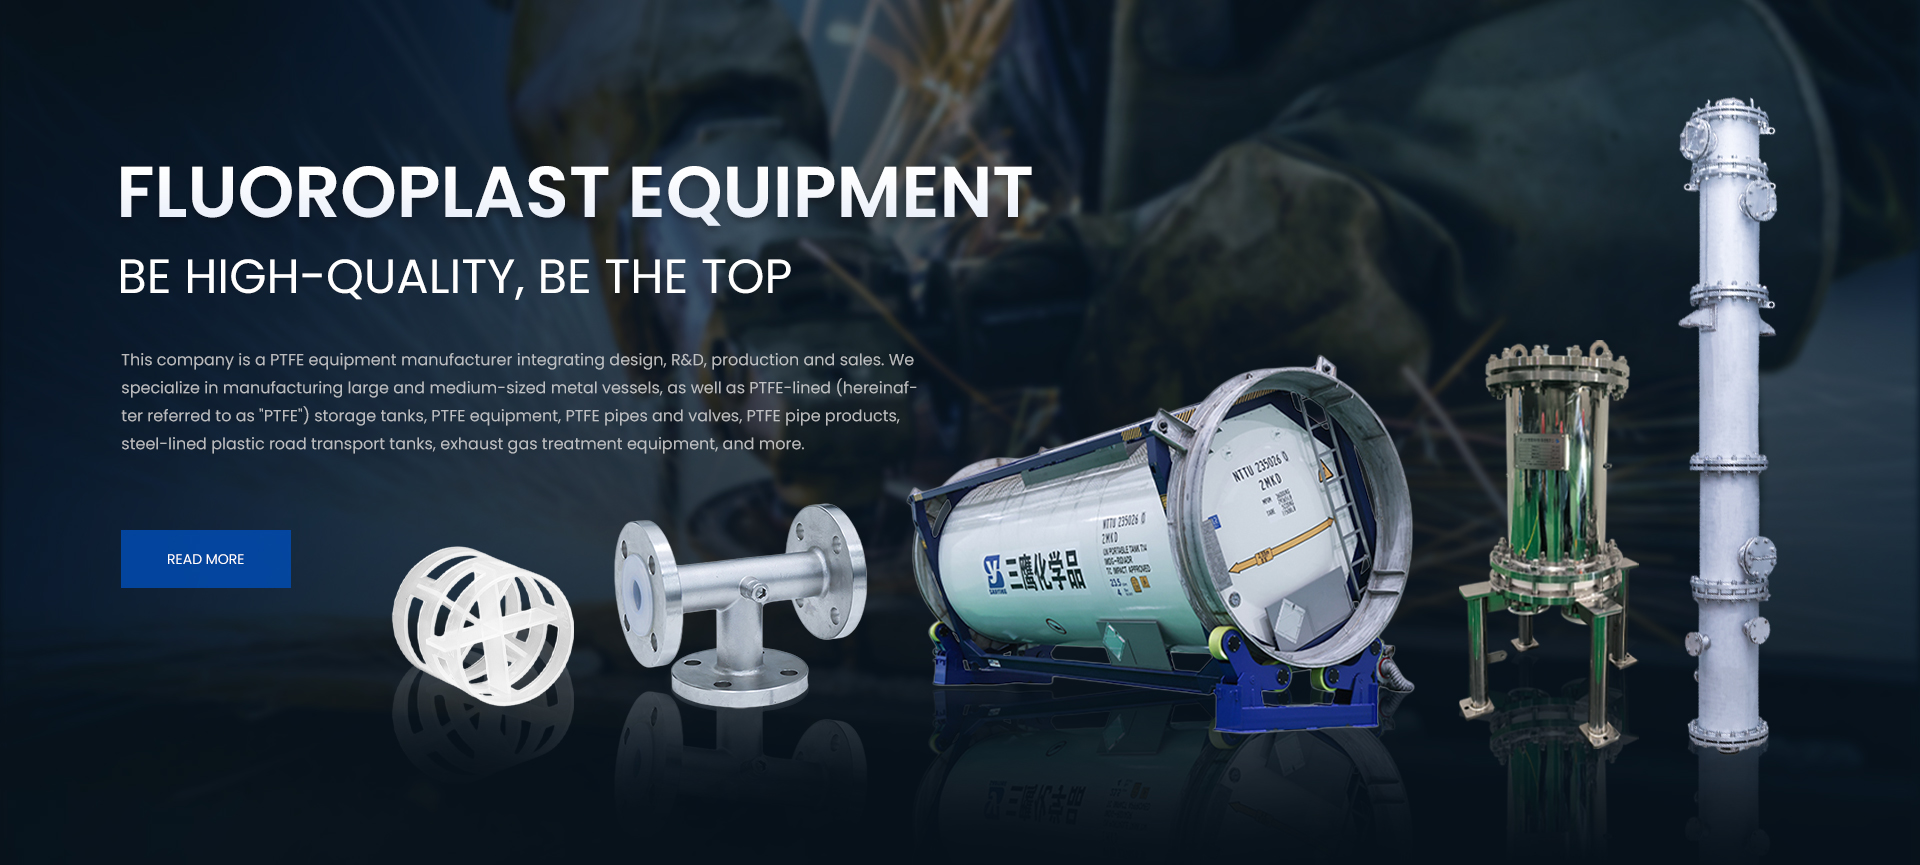
This guide explains how ptfe equipment and storage tanks is tested, which standards apply, what certification actually proves, and how buyers can verify quality before, during and after production. It reflects the practices at æ±èæ·åæ°æææéè´£ä»»å ¬å¸ (www.jsjcxclgs.com).
Suppliers make broad quality claims. These are the specific questions that turn a claim into evidence.
Which standard, exactly? Ask for the standard number, not a general assurance.
Who issued the certificate? Recognised third-party bodies carry more weight than self-declarations.
What is the scope? A certificate may cover only part of the product range.
Is it current? Check validity dates and renewal status.
What is the incoming inspection protocol? Ask for the checklist and sampling plan.
What happens when a defect is found? A defined corrective process matters more than a zero-defect promise.
A quality management system (QMS) is the documented set of processes that control how a product is made, inspected and released. Certification such as ISO 9001 confirms that the system exists and is audited; it does not by itself guarantee product quality, but it makes quality repeatable.
Incoming material control: verifying raw materials against specification before use.
In-process control: checking parameters and dimensions during production.
Final inspection: verifying finished goods before packing.
Corrective action: investigating and fixing root causes of defects.
Buyers should treat a QMS as a foundation. On its own it is necessary but not sufficient; it must be paired with genuine product testing.
Different products require different tests, but the categories are consistent across manufacturing:
| Test Category | What It Verifies | Typical Method |
|---|---|---|
| Dimensional | Size and tolerance | Caliper, gauge, CMM |
| Functional | Performance under load | Bench and endurance testing |
| Material | Composition and grade | Spectrometry, certificate review |
| Safety | Compliance with standards | Type testing, Hipot, pressure test |
| Environmental | Resistance to conditions | Humidity, temperature, salt spray |
Ask which of these are performed routinely and which only on request. A factory that tests every batch is fundamentally different from one that tests only the first sample.
Certification confirms that a product or process has been assessed against a standard by an accredited body. It is a valuable signal, but it is not a guarantee of every unit.
Proves: the tested sample complied with the standard at the time of testing.
Does not prove: that every production unit complies, or that the factory maintains the same process over time.
Best practice: combine certification with routine batch testing and periodic re-verification.
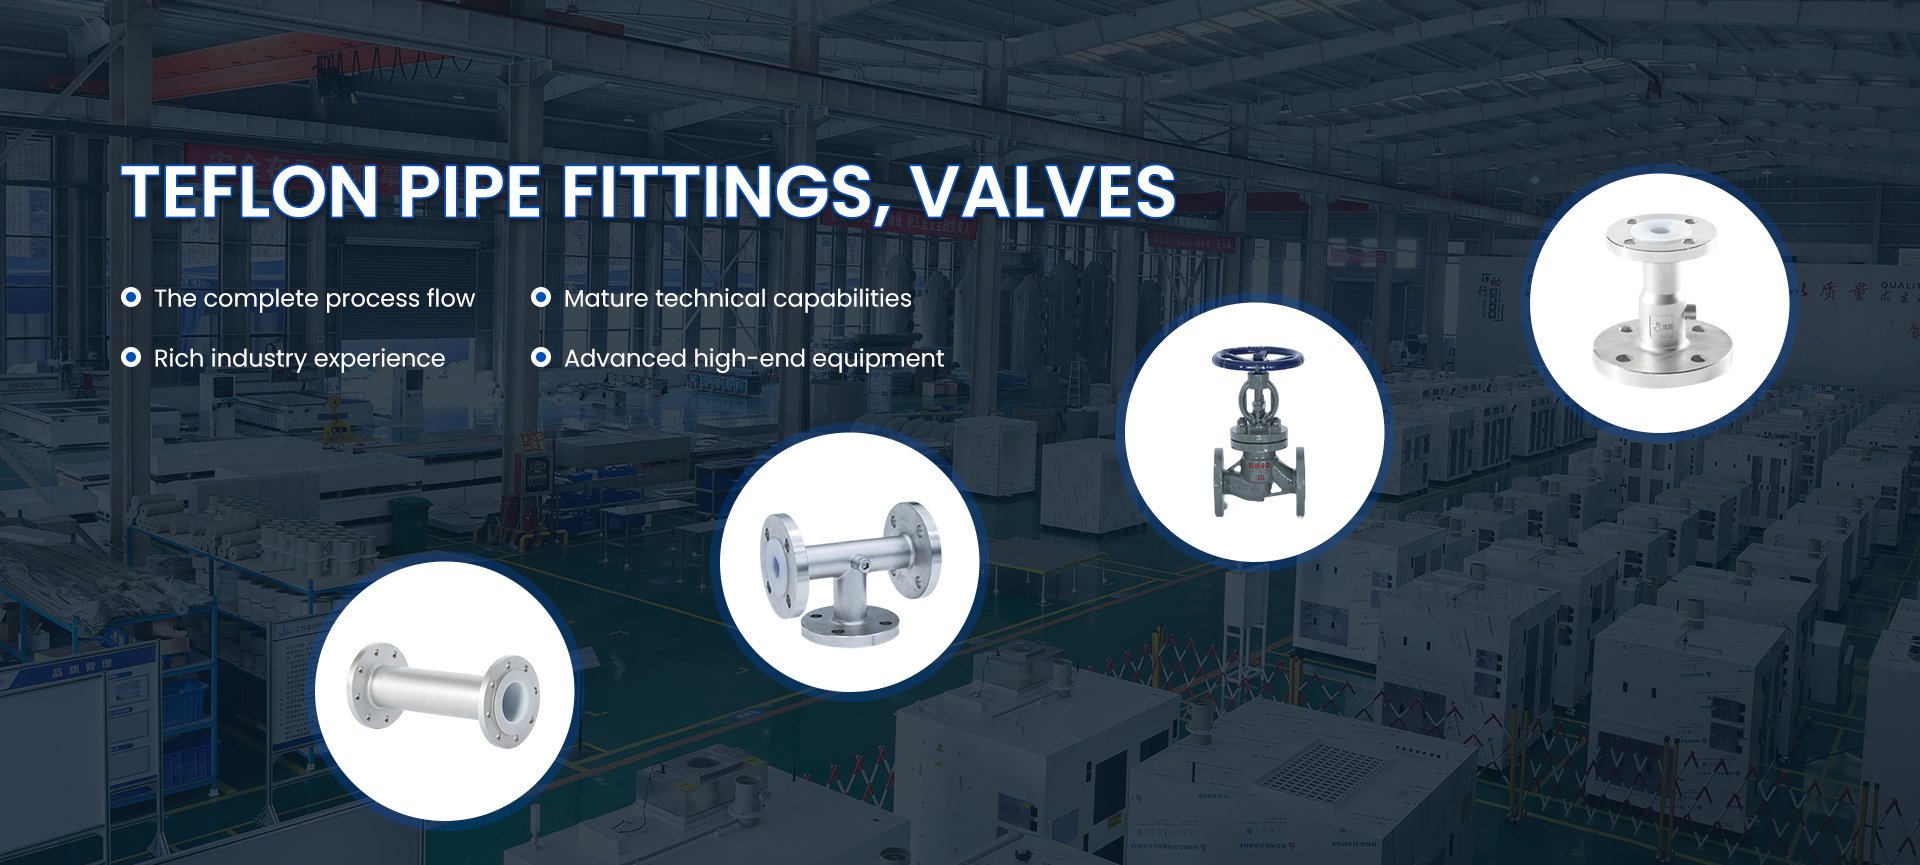
For ptfe equipment and storage tanks, the relevant certifications typically include ISO 9001, CE. Confirm the scope of each certificate covers the exact product you are buying.
A simple incoming inspection protocol is the buyer's last line of defence. It is inexpensive and catches the majority of problems before they reach customers.
Sample the shipment according to a defined plan (for example, per pallet or per batch).
Measure the key specification parameters and record the results.
Functionally test a representative subset.
Verify labelling, packaging and documentation against the approved artwork.
Document results by batch number and raise trends with the supplier.
Reject or negotiate remedies for any lot that fails the criteria.
Keep the data. A buyer who can show three months of measured results has far more leverage in a quality conversation than one who reports only that a batch felt wrong.
Understanding why quality varies helps buyers ask better questions.
Raw material substitution: lower-grade material used to reduce cost.
Tool wear: moulds and dies degrade and produce out-of-tolerance parts over time.
Process drift: settings change without documentation.
Operator variation: manual steps introduce inconsistency.
Sub-supplier quality: components from third parties may not meet the same standard.
A factory that monitors these factors proactively prevents most defects before they occur.
Put quality terms in the contract, not just in conversation. Specify the standard, the sampling plan, the acceptance criteria, the remedy for non-conformance, and the documentation you expect with each shipment.
This protects both sides. The supplier knows exactly what is expected, and you have a defined basis for discussion if something goes wrong.
Recurring quality management means tracking a small set of metrics rather than reacting to individual complaints.
| Metric | What It Measures | Target | Action If Breached |
|---|---|---|---|
| Defect rate | Share of units failing inspection | < 1% | Investigate root cause with supplier |
| On-time delivery | Shipments meeting the agreed date | > 95% | Review capacity and planning |
| First-pass yield | Units passing without rework | > 98% | Analyse process weak points |
| Warranty claim rate | Field failures under warranty | < 2% | Reassess design and testing |
| Documentation accuracy | Correctness of shipping paperwork | 100% | Tighten release checklist |
Track these monthly and review them with the supplier quarterly. A small set of well-understood metrics beats a large set of ignored reports.
The applicable standards depend on your destination market and product category. These are the ones most commonly requested.
ASTM D3294: verify the factory can supply the current certificate and that its scope covers your product.
ISO 9001: verify the factory can supply the current certificate and that its scope covers your product.
GB standard: verify the factory can supply the current certificate and that its scope covers your product.
CE: verify the factory can supply the current certificate and that its scope covers your product.
ISO 9001: request the certificate and confirm validity.
CE: request the certificate and confirm validity.
This is the workflow that turns a quality policy into shipped quality.
Approve the specification and the golden sample in writing.
Verify incoming materials against certificates.
Control in-process parameters and record them.
Run functional and safety tests at defined intervals.
Perform 100% or AQL final inspection before packing.
Complete a pre-shipment inspection with photographic records.
Archive the batch documentation for traceability.
Feed field performance back into design and process improvement.
The two inspections answer different questions, and only one of them can still save the order:
| Checkpoint | What It Catches | What Final Inspection Catches of the Same Problem |
|---|---|---|
| Incoming material check | Wrong grade, substituted material, expired stock | Nothing â the defect is welded into the finished unit by then |
| First-article review | Setup errors, wrong programme, fixture mistakes | A full production run of the same error, discovered at the end |
| Mid-run audit | Drift, tooling wear, operator shortcuts accumulating | The defect rate itself, plus the scrap already produced |
| Pre-pack check | Missing accessories, wrong counts, damaged units | The same items â this is the checkpoint final inspection duplicates |
| Documentation mid-check | Certificates mismatched to batch numbers | A packed, sealed problem that stops at customs instead |
The economics are blunt: a defect caught at intake costs the price of the material; caught at first article, the price of a shift; caught mid-run, the price of rework; caught at final inspection, the price of the unit; caught by your customer, the price of the relationship. In-process inspection is not extra inspection â it is the same budget moved to where each unit of attention buys the most. Specify the checkpoints in the quality annex, require evidence at each gate rather than a promise of it, and let the final inspection shrink to a sampling confirmation rather than the programme's only defence.
A certificate confirms compliance with a standard following assessment by an accredited body. A test report records the results of specific tests. Both are useful; the certificate is a higher-level signal, while the report gives detail.
ISO 9001 confirms that a documented quality management system is in place and audited. It makes quality repeatable but does not by itself guarantee a specific product's performance. Combine it with product testing.
Most buyers re-audit annually, or more often if the supplier is new, critical, or has had recent quality issues. Periodic third-party testing complements internal audits.
Document the failure with evidence, notify the supplier formally, and agree a remedy â rework, replacement, credit or return. Track the resolution to confirm the root cause is fixed.
Yes, and it is good practice. Many buyers appoint a third-party inspection company to verify goods before they leave the factory.
It depends on the market: CE for the EU, UL or ETL for North America, and specific standards for food, medical or electrical applications. Confirm the requirement for your destination before ordering.
Check the issuing body's database, confirm the certificate number, scope and validity, and ensure the product in question is covered.
Broadly, yes â but not perfectly. A structured audit and batch testing reveal real quality differences that price alone cannot.
Most quality surprises are born as ambiguity, and most ambiguity is born as a sentence that read perfectly in one language and meant something adjacent in another. The discipline is structural, not linguistic â write instructions the way a careful stranger would need them:
One instruction, one action: compound sentences compound errors; 'seal and label each carton' produces cartons that are sealed but unlabelled, or labelled twice.
Numbers over adjectives, always: 'tighten firmly' becomes 'tighten to 25 Nm' the moment you write the specification instead of the vibe.
Referenced visuals: a diagram with an arrow outlives any paragraph; photograph the correct result and attach it to the sentence that demands it.
Confirm-back protocol: the receiver restates the instruction in their own words before production â the restatement is where the misunderstanding shows up, while it is still free.
One channel, one version: instructions distributed across chat threads, emails and phone calls merge into folklore; the numbered, dated master document attached to the PO is the only version that counts.
Test the system once per supplier: deliberately include one harmless instruction whose only virtue is clarity, and see whether the result matches the words. Suppliers also read the discipline as a signal â a buyer whose instructions are precise, referenced and confirmed-back is managed differently from one whose orders arrive as mood. The writing time is minutes; the claims it prevents are measured in containers.
The cheapest quality checkpoint in any factory is the one at material intake, and the cheapest of all is a specification that tells intake what to check. The controls worth requiring for your orders:
| Control Point | What It Prevents | Evidence to Require |
|---|---|---|
| Material certificate against specification | Wrong grade or substituted raw material arriving as 'equivalent' | Mill certificates naming grade, batch and standard edition â matched to the delivery, not to the file |
| Batch quarantine on arrival | Mixed or aged stock entering production untracked | Quarantine zone with status tags photographed at receipt |
| First-batch physical sample retained | Disputes later about what the material actually was | A retained, dated, labelled sample per batch â the reference that ends the argument |
| Supplier-of-supplier changes flagged | Silent upstream substitution that shifts performance | A change-notification clause in the material purchase, enforced by spot checks |
| Expiry and storage conditions | Degraded adhesives, coatings and compounds entering production | Storage records for time-sensitive materials; wall-clock dates, not memories |
Inspect the intake area on any factory visit before you inspect anything else â the discipline visible there predicts the discipline everywhere else, because intake is where shortcuts are cheapest and least observed. Buyers who add an intake-verification clause to their quality agreement, with evidence required per batch, convert the vaguest part of quality into a document trail. The factories that resist the clause have told you something; the ones that already run it have told you something better.
The meeting happens after the deposit and before the first machine runs, with the people who will actually run production â not the salesperson who sold it. The agenda that fits the hour:
Walk the specification, line by line (20 min): every drawing revision, tolerance and finish confirmed against the golden sample in the room â ambiguities surface here for free instead of later as claims.
Confirm the inspection plan (10 min): which checkpoints, what evidence at each, who does the checking, and what happens on a fail â agreed while both sides are still cooperative by reflex.
Fix the change-control rule (5 min): any deviation, however small, requires written approval before production continues â the rule that prevents the well-meant substitution.
Set the communication rhythm (10 min): production update dates, named contacts on both sides, and the escalation path for the questions nobody wants to ask.
Write the summary before leaving (15 min): one page, signed, attached to the order â the meeting's product is the page, not the feeling.
Run it once per new product and once per major revision; experienced pairings compress it to twenty minutes on the phone. The meeting's quiet value is calibration: you learn how the factory thinks, they learn how seriously the specification is read, and the order runs on a shared page instead of two confident assumptions. The hour is the least expensive quality investment in the entire cycle â and the one most often skipped by buyers who later spend a month writing claims.
Negotiations are won in preparation and merely held in the room. The pack that serious buyers assemble before any consequential supplier meeting fits in six pages and changes the tone of everything said on top of it:
The numbers page: order history, on-time-in-full, quality cost and claim ledger for the relationship â your copy matches what you would show them, which is why it carries weight.
The market page: current input-price movement, freight trend, and one anonymised competing quotation â context, not threat.
The asks page: your three requests ranked, each with what you are offering in exchange; buyers who arrive with asks and nothing to trade negotiate against themselves.
The walk-away page: your real alternative, priced and dated â written before the meeting, when arithmetic is calm, not during it.
The concessions ladder: what you can give, in what order, and the floor beneath which nothing moves â agreed internally so the meeting negotiates with the supplier instead of with your own side.
Circulate the pack to your own side only, and brief everyone attending on the ladder â internal surprise is the most common cause of a concession nobody authorised. After the meeting, append the outcomes and file it: the pack becomes the relationship's running record, and next year's preparation starts from evidence instead of recollection. Suppliers notice preparation and price accordingly â the meeting with a prepared buyer is shorter, more specific and rarely revisited.
Individual inspection reports answer 'was this shipment acceptable'; a trend ledger answers the question that actually manages a supplier â 'in which direction is quality moving, and why'. The ledger is one table, updated per shipment:
| Ledger Column | What It Records | What It Reveals Over Time |
|---|---|---|
| Shipment defect rate | Major + minor defects as a percentage against AQL, per shipment | Drift long before a failure: two consecutive rises outrank any single bad report |
| Defect class mix | Which defect types recur â finish, dimension, function, packaging | A structural cause: the same class recurring points at process, not chance |
| Corrective-action closure | Days from CAR raised to evidence accepted | Whether the supplier fixes causes or closes paperwork |
| Re-inspection outcome | Pass rate of shipments that failed first inspection | True process control â a high re-pass rate means the first failure was noise; a low one means it was signal |
| Season or batch context | Production month, batch size, operator notes from the factory | Patterns the factory will recognise: new staff, material lots, holiday-season shortcuts |
Review the ledger quarterly and bring it to the supplier â the conversation shifts from anecdote to arithmetic, and factories respond to their own trends with engineering rather than apology. The ledger also disciplines your own claims: patterns visible across shipments justify the deeper audit, the tighter checkpoint or the second source, while isolated bad shipments justify exactly what they cost. Quality management without a trend line is memory; memory in procurement, as elsewhere, is systematically kind to the recent shipment and cruel to the annual budget.
Freight invoices arrive after the cargo, against memories that have moved on â which is precisely why they are worth reconciling. The audit takes minutes per shipment and catches a category of leakage nobody budgets for:
Match the quotation first: rate, surcharges, currency and validity date â quotes expire quietly, and expiry is the most common origin of an 'increase' nobody agreed.
Check the weight and volume basis: billed versus verified; volumetric conversions and rounding rules differ between carriers and between invoices from the same one.
Scrutinise the surcharge lines: fuel, congestion, handling, documentation â each should map to the quotation's terms; new names on an invoice are new charges, not new facts.
Verify the accessorials: storage, exam attendance, detention â the charges that appear when something went wrong, priced against who actually caused the wrongness.
Log every dispute and its outcome: the pattern across invoices is the real negotiation â a forwarder's billing accuracy is a scorecard line, and it should be scored.
Run the audit on every invoice or sample one in three where volumes make that rational â the discipline, not the coverage, is what changes forwarder behaviour. Dispute within the window, in writing, with the quotation attached; most discrepancies settle immediately because nobody upstream expected them to be noticed. The audit's quiet effect is pricing integrity: forwarders bill their most accurate invoices to the buyers who read them, which makes the audit one of the better hourly rates in procurement.
Usually yes, in structure: knowing their share is capped makes the supplier compete on service within a defined role instead of campaigning for the whole volume, and it removes the anxiety that produces aggressive pricing 'while they still have you'. What you keep private is the identity of your primary and the exact split. Suppliers in a genuine dual-source programme behave measurably better on responsiveness â competition does the managing that no scorecard meeting achieves.
Two to three is the healthy range: one to evaluate capability, one to confirm corrections, optionally one to confirm the confirmed. One round is rarely enough for anything custom â it samples the factory's ambition, not its process. More than four usually signals a specification problem being passed back and forth: stop sampling, rewrite the specification with numbers and reference photos, then sample once against the rewritten version. Sampling without a changing specification is not due diligence; it is a subscription.
The pre-agreed rule decides, not the argument â which is why the rule belongs in the quality annex. The market convention: re-inspection and rework after a genuine fail are the supplier's cost; your inspector's travel for the re-check is negotiable but commonly the supplier's too where the fail was severe; and disputes about whether it failed at all are priced by the third-party report, shared or supplier-borne per your terms. Buyers without a written rule pay for failures twice â once in defects and once in the negotiation about them.
Only with written permission, and the permission should name scope and term. Beyond the legal question sits the strategic one: catalogue content shared across an industry makes your site indistinguishable from the next reseller's, and search engines increasingly reward originality. Negotiate content rights as part of the first order â most suppliers grant them for their customer â then invest in your own photography and measurements for the products that matter. The page that describes the product in your words, with your images, sells for years; the borrowed page sells for everyone equally.
Specifically and promptly: one short message stating the decision, the deciding factor and whether they should quote future tenders. 'Your price was above alternatives by roughly X on like-for-like scope' is a sentence suppliers can act on and remember; silence is one they file. The suppliers you decline well return with better offers and better behaviour â the market is smaller than it looks, and today's declined quote is next year's benchmark or backup. Declining badly costs nothing today and a network later.
Scorecards are filed; feedback letters are read. Once a year, send each significant supplier a one-page letter â signed by the decision-maker, not the day-to-day contact â that states three things: what the supplier did well in concrete, quotable terms; the one or two areas where performance fell short of the standard, with the numbers attached; and what the relationship will be tested on in the coming year, stated as observable facts rather than hopes. The format forces precision on both sides â praise without evidence is noise, criticism without numbers is mood, and a forward plan without observable criteria is a wish. Suppliers respond to the letter disproportionately: it is rare, it is specific, and it comes from someone with authority. File the reply, act on the commitments it contains, and let next year's letter open with last year's â the sequence of letters becomes the relationship's biography, and the biography becomes the cheapest management tool you own.
If you want to see how quality is controlled in practice, æ±èæ·åæ°æææéè´£ä»»å ¬å¸ (www.jsjcxclgs.com) is happy to share inspection records, test reports and certification for our ptfe equipment and storage tanks. Visit www.jsjcxclgs.com to learn more and request documentation for your market.
पता: नंबर 1, जिंगपोहू सड़क, सुसु औद्योगिक क्षेत्र, सुकियान शहर, जियांग्सू प्रांत, चीन
स्यू हाओ: +86 13813955525
स्यू गांग: +86 15189058237
ईमेल: zhaojiguang@jsjcxcl.com.cn


कॉपीराइट © 2023 जियांग्सू जिचुआंग न्यू मटेरियल्स कं, लिमिटेड साइट मैप
यह वेबसाइट यह सुनिश्चित करने के लिए कुकीज़ का उपयोग करती है कि आपको हमारी वेबसाइट पर सर्वोत्तम अनुभव मिले।

 English
 Pусский
 日本語
 한국어



 Whatsapp
 टेलीफ़ोन
टिप्पणी
(0)